As a seasoned specialist with nearly a decade of experience in resource regeneration, I still recall the striking scene when I first stepped into a warehouse for spent batteries. Tons of retired power lithium batteries and 3C consumer batteries piled up like hills. Damaged casings leaked electrolyte, leaving dark stains on the floor. Amid mixed metal frames and plastic shells, partially discharged cells glowed faintly.
That moment made it clear: lithium battery recycling and disassembly is far more than simple scrap disposal. It demands precise control over chemical energy and mechanical force, and carries the mission of environmental protection and resource conservation. Drawing on years of hands-on project experience, we have developed this practical, replicable battery recycling and disassembly process solution.
1. Project Background & Targets
1.1 Industry Drivers
Driven by booming new-energy vehicle ownership and rapid iteration of 3C electronics, millions of tons of end-of-life lithium batteries are retired annually. Direct landfilling allows lithium, cobalt, nickel and other heavy metals in electrolyte to contaminate soil and groundwater. Simple incineration releases toxic fluorides and VOCs that pollute the atmosphere.
More importantly, the domestic industry relies heavily on imports for lithium, cobalt and nickel. Tapping these “urban mines” is not only an environmental necessity, but also a strategic priority for resource security.
In one retired power battery project we delivered in the early stage, crude disassembly processes yielded copper-aluminum separation efficiency below 60% and lithium recovery rate of only 55%. Large quantities of valuable metals were contaminated by impurities and sold at discounted prices. This proves that the refinement level of disassembly technology directly determines the commercial value of recovered materials.
1.2 Core Objectives
Our solution is built on three pillars: Safe Operation, High Resource Recovery & Eco-friendliness.
- Safety: Zero safety incidents. Strict risk control against short-circuit ignition, electrolyte leakage and volatile toxic fumes.
- Resource Recovery: Comprehensive recovery rate of key metals (lithium, cobalt, nickel, copper, aluminum) ≥95%; recovery rate of non-metallic fractions including plastics and separators ≥85%.
- Environmental Compliance: 100% qualified treatment of waste gas, wastewater and solid residues. Dust-free workshop environment with odor kept below the sensory threshold.
2. Full-Process Disassembly Workflow
The whole workflow follows a progressive sequence: Pretreatment → Precision Disassembly → Deep Sorting → Post-processing. Every stage is closely linked, similar to sophisticated surgical operation on batteries. We focus not only on successful cell opening, but also high-accuracy material segregation.
2.1 Pretreatment: The First Safety Barrier
Pretreatment acts as the safety gate of the whole production line. It addresses two core hazards: eliminating residual electric energy inside cells and stripping outer protective structures.
(1) Discharge Treatment Retired batteries normally retain 10%–30% residual charge, which may trigger short-circuit and fire if disassembled directly. We adopt combined physical and chemical discharge: batteries are immersed in sodium chloride conductive solution (5%–8% concentration) for slow energy release. After cell voltage drops below 1 V, pulse discharge equipment is used for precise deep discharge until voltage stabilizes under 0.5 V.
We once handled a batch of 18650 cylindrical cells. Incomplete pre-discharge caused one cell to spark during disassembly, nearly igniting surrounding plastic components. Since then, we enforce double discharge verification: technicians measure voltage at no less than three test points with a multimeter before releasing any batch for downstream processing.
(2) Casing Stripping Battery casings are mostly aluminum or steel. Tools are selected by battery form factor. Prismatic cells are cut along weld seams by hydraulic shears; cylindrical cells are circumferentially sliced by rotary blades; pouch cells are heated on hot plates to soften sealing adhesive before casing removal.
Extreme care is required to avoid piercing internal cells. Improper shear pressure once ruptured a cell, causing electrolyte splash onto the operator’s face shield. Operators are now required to wear acid-alkali resistant gloves and safety goggles, and all machines are fitted with emergency stop buttons.
2.2 Precision Disassembly: Layer-by-Layer Separation
After pretreatment, we move to core disassembly. A lithium cell resembles a sandwich: outer casing, internal cell core (wound or stacked cathode sheets, anode sheets and separators), busbars and BMS control systems. Disassembly follows the sequence: outside-in, coarse-to-fine.
(1) Mechanized disassembly supplemented by skilled manual work Our custom disassembly line uses mechanical grippers to fix battery packs, rotary clamps to remove end plates, and pneumatic pushers to eject modules. For complex designs such as blade batteries, experienced technicians disassemble screws and manually separate busbars and cells.
We once processed retired packs from an automaker with densely routed BMS wiring. Robotic arms failed to separate the circuit boards accurately. Senior operators completed the delicate stripping with magnifiers and tweezers over three hours. It reminds us that even advanced automation relies on skilled human calibration.
(2) Cell-type targeted processing Disassembled cells are sorted into cylindrical, prismatic and pouch types. Cylindrical cells are longitudinally split by roller crushers to expose electrode sheets; prismatic cells are split along edges with hydraulic chisels; pouch cells are opened with thermal knives to melt aluminum-laminated film seals for electrode roll extraction.
Force control is critical: insufficient force fails to open cells, while excessive force shreds foils and compromises subsequent sorting. Our disassembly technicians complete one-month hands-on training on scrap cells, learning to judge proper cutting effect by the crisp cracking sound.
2.3 Deep Sorting: Material Purification Stage
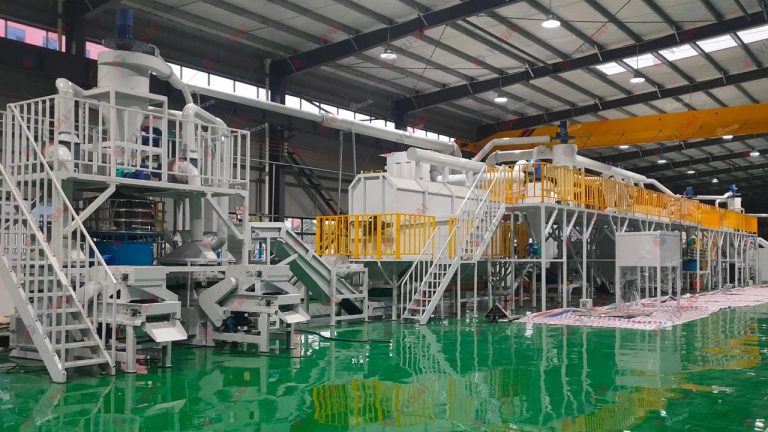
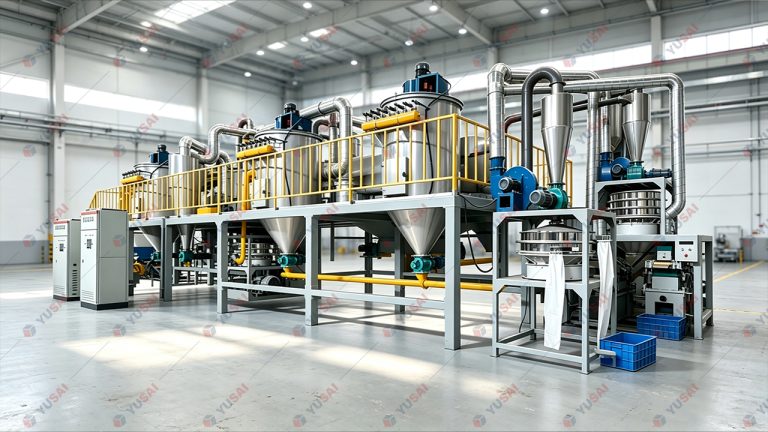
Disassembled output is a mixed stream: steel / aluminum housings, copper busbars, plastic brackets, mixed anode & cathode sheets carrying LCO and graphite active materials, separators and residual electrolyte. Sorting separates every material fraction for dedicated recovery routes.
(1) Structural component sorting Steel and aluminum shells are separated via magnetic separator (ferromagnetic steel vs non-magnetic aluminum) plus eddy current separator (aluminum vs plastic). Copper bars and nickel tabs are manually picked by color distinction. Plastic brackets are separated by gravity / density sorting: PP and ABS float in water while PBT sinks.
Trace cross-contamination downgrades final material quality, e.g. copper impurities mixed in aluminum scrap reduce recycled aluminum grade. We implement three-stage sorting: primary mechanical separation → manual re-inspection → final check via metal detectors.
(2) Electrode sorting and active material liberation Anode and cathode sheets are stacked with separators in between. High-speed air classification removes lightweight separators. Remaining electrode sheets go through magnetic roller + electrostatic separation: anode (copper foil + graphite) is weakly magnetic and captured by magnetic rollers; cathode (aluminum foil + lithium cobalt oxide) is non-magnetic and conveyed forward.
Separated electrodes enter crushing and screening units. Materials are crushed below 2 mm. Ductile copper and aluminum foils remain flaky while active powders turn fine, and the two streams are separated by vibrating sieve. At early commissioning, graphite dust spread heavily across the workshop. Pulse dust collection systems were installed to resolve the dust issue.
2.4 Post-processing: Final Step for Value Upgrading
Sorted materials require further purification before closed-loop recycling. (1) Metallic material refining Cleaned aluminum shells and copper busbars are melted and cast into standard ingots. Lithium cobalt oxide powder goes through acid leaching (sulfuric acid + hydrogen peroxide), solvent extraction (P204 for impurity removal, P507 for cobalt-nickel separation) and precipitation (sodium carbonate for lithium precipitation), yielding lithium carbonate and cobalt sulfate. Graphite powder is calcined at high temperature to remove binders, milled and classified to produce regenerated graphite anode material.
(2) Non-metallic material treatment Cleaned separators are recycled as low-grade plastic feedstock. Residual electrolyte is adsorbed by activated carbon; saturated carbon carriers are sent to licensed hazardous waste disposal facilities. Process wastewater mainly contains sodium chloride and trace heavy metals. It is neutralized with sodium hydroxide to pH 8–9 for heavy metal precipitation, then treated by reverse osmosis membrane filtration. Treated water meets discharge standards and is recycled onsite.
3. Key Technology & Quality Control
3.1 Core Technical Advantages
High recovery performance is supported by three proprietary innovations:
- Multi-chemistry compatibility: Adapted for NMC ternary, LFP lithium iron phosphate and LMO lithium manganate batteries. Cutter material is adjusted accordingly (hard alloy for hard ternary cells, high-speed steel for brittle LFP). Discharge duration is extended by 30% for slow voltage decay of NMC batteries.
- High-efficiency electrode separation: Self-developed electromagnetic-airflow coupled sorter lifts cathode-anode sorting accuracy from 85% up to 98%, recovering roughly 20 extra tons of copper and aluminum annually.
- Electrolyte emission control: Negative pressure ventilation system (air velocity ≥0.5 m/s) equipped in disassembly zones with overhead activated carbon adsorption units cuts volatile electrolyte release by 90%, drastically reducing workshop irritant odor.
3.2 Full-Line Quality Control System
Quality is the foundation of recycling profitability. We adopt a three-phase QC framework:
- Incoming inspection: Identify battery chemistry, voltage, weight and visual damage. Segregated storage for damaged cells to avoid electrolyte cross-contamination.
- In-process inspection: Material samples are tested every two hours. XRF spectrometer verifies copper & aluminum purity (target ≥99%). Electronic weighing tracks active material recovery (target ≥95%).
- Finished goods inspection: Regenerated products undergo full testing. Lithium carbonate is checked for main content (≥99.5%) and impurities (sodium ≤0.02%). Regenerated graphite is tested for specific capacity (≥340 mAh/g) to comply with recycled material standards.
4. Safety, Environmental Compliance & Occupational Health
4.1 Safety Protection Framework
Battery disassembly zones carry high risks. We implement dual safeguards of hardware and management protocols:
- Hardware: Explosion-proof lighting, combustible gas detectors for hydrogen and methane, fire sand bins for small fire suppression, emergency showers for electrolyte splash flushing. Disassembly machines have overload protection and emergency stop buttons; discharge stations are isolated in dedicated containment rooms.
- Management: Three-tier training program (site safety induction → operational training → emergency drill). Monthly fire drills simulate battery fire scenarios. Third-party safety audits are arranged quarterly.
4.2 Environmental Compliance
Environmental compliance is mandatory rather than optional. 90% of treated wastewater is reused for battery discharge; 10% is discharged after reaching standard. Waste gas passes through spray scrubbers (dust removal) + activated carbon adsorption (VOC removal), with emission concentrations far below regulatory limits. Spent activated carbon and heavy-metal sludge are transferred to certified hazardous waste handlers; ordinary solid waste such as packaging cartons is sold for recycling.
4.3 Occupational Health Management
Frontline operators are our most valuable asset. We supply acid-resistant gloves (≥8-hour resistance to sodium hypochlorite), full-face respirators (≥95% filtration efficiency for 0.3 μm particulates), and anti-puncture safety footwear. Monthly occupational health examinations cover blood lead and cadmium tests. Nutritional supplements are distributed quarterly to reduce health burdens from chemical exposure.
5. Summary & Outlook
This process solution evolves from years of practice, shifting our operation from “disposing defective batteries” to “recovering valuable resources”. Every end-of-life battery is fully utilized. It is deeply rewarding when regenerated lithium carbonate is delivered back to battery manufacturers and becomes power cores for new EVs.
As sodium-ion batteries and solid-state batteries gain market penetration, disassembly technologies will keep evolving. However, our core principle remains unchanged: safety first, resource maximization and environmental stewardship. With rigorous technical standards and respect for nature, spent lithium batteries will transform from environmental liabilities into sustainable green mineral resources.