With the widespread popularity of new energy vehicles, energy storage equipment and digital electronic products, a large number of retired lithium-ion batteries have entered the end-of-life cycle. Waste lithium-ion batteries are environmentally hazardous solid waste, while also being known as “urban mines” rich in lithium, nickel, cobalt, manganese, copper and aluminum resources. Building a safe, high-recovery and environmentally compliant lithium-ion battery recycling production line has become an essential demand for resource recycling enterprises and industrial park projects.
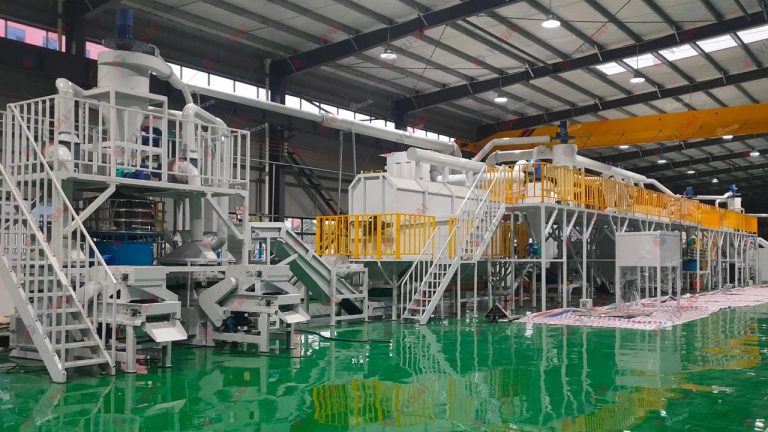
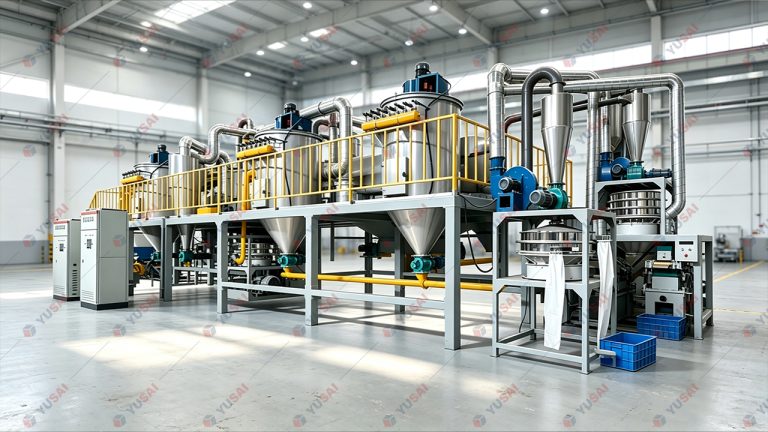
As a professional manufacturer with decades of experience in equipment R&D and manufacturing, we provide a full set of modular turnkey overall solutions for lithium-ion battery recycling plants. Our one-stop service covers process design, equipment manufacturing, complete system integration, installation and commissioning, personnel training and lifelong after-sales technical support. Clients can launch lithium battery recycling projects efficiently without coordinating with multiple suppliers.
Applicable Processing Materials
The production line is compatible with lithium battery materials in various forms and systems:
-
Pouch, cylindrical and prismatic power batteries (EV batteries)
-
3C consumer lithium batteries for digital products
-
NCM/NCA ternary lithium batteries and LFP lithium iron phosphate batteries
-
Battery pole piece scraps and electrode waste materials from battery factories
Main Output Products
Through crushing, pyrolysis, multi-stage magnetic separation and air gravity separation processes, the line directly produces marketable finished materials, including black mass, copper granules, aluminum granules, steel shells and separator films. Equipped with an optional hydrometallurgy refining system, the black mass can be further purified into battery-grade lithium hydroxide, nickel sulfate, cobalt sulfate, manganese sulfate and lithium carbonate, which can be directly supplied to cathode material manufacturers.
Core Technical Advantages
Ultra-high Recovery Efficiency: The comprehensive recovery rate of metals and black mass reaches over 98%. The produced black mass features low impurity content, greatly improving the market value of recycled materials.
Modular and Flexible Design: The entire production line adopts modular units, which can be flexibly configured according to customers’ planned production capacity and site space. Custom solutions are available from small pilot lines to 10,000-ton industrial production lines.
Safe and Closed Production Process: The crushing and pyrolysis sections adopt a closed negative pressure design, equipped with a complete tail gas purification system to treat organic volatile matters such as electrolytes and binders. It fully meets environmental emission standards of various regions and effectively avoids battery fire and explosion risks.
Full-process One-stop Turnkey Service: We provide full lifecycle services including pre-project consultation, equipment selection, drawing and scheme design, equipment processing and manufacturing, on-site installation and commissioning, equipment operation and maintenance, and lifelong after-sales technical support.
Our Manufacturing Strength
Our company owns a professional technical R&D team of more than 30 members, with an annual R&D investment accounting for 6% of annual revenue. The factory is equipped with over 60 sets of mechanical processing equipment, supporting complete production capabilities including cutting, forming, welding, painting, assembly and commissioning. We support OEM and ODM customized development, providing mature and tailored recycling process equipment for global clients.
Whether you plan to build a new lithium battery pre-treatment production line or add a back-end hydrometallurgy refining unit, we can deliver professional and mature technical solutions matching your material characteristics and investment budget.